
Conveyor System Integrator
RMH Systems designs and integrates custom conveyor systems that keep products moving efficiently through your operation.
Whether you need to move individual products, cases, pallets or heavy loads, your system is designed around your throughput, facility and process. From a single conveyor line to complete automation, you get the experience of thousands of conveyor systems implemented nationwide.
Talk with a Material Handling Expert
Specializing in Complete Conveyor System Integration
Conveyors are only one part of a much larger automated system. As a conveyor system integrator, RMH incorporates the equipment, controls and automation expertise to move products through your operation through one solution.
Here’s how we can help you work smarter and more efficiently.
✓ System Design & Engineering: Plan conveyor layout, equipment and material flow around your products, throughput and facility.
✓ Equipment Integration: Connect conveyors with packaging equipment, palletizers, storage systems and other automation.
✓ Controls & Programming: Integrate controls and programming so equipment communicates and operates as one system.
✓ Installation & Startup: Coordinate installation, system integration, testing and startup.

Conveyor Systems Built Around What You Move

Products & Packages
Cases, cartons, totes, and individual products.
Pallets & Heavy Loads
Pallet movement and heavy-duty material handling.

Food & Beverage
Washdown, sanitary, and food production applications.

Specialty & Custom
Unique products, processes, layouts, and handling requirements.
Case & Product Conveying
Move cases, cartons, totes, packaged goods, and individual products through your operation.


Pallet & Heavy-Duty Conveying
Transport palletized loads and other heavy products throughout your facility.

Turntable Conveyors
Rotate and redirect palletized loads in tight spaces. Integrates with CDLR and chain conveyors.

Conveyor Systems by Industry
We design conveyor systems for a wide range of companies, but these are some of the industries we work with most often.

Food Manufacturing
Sanitary conveying, washdown applications, packaging-line integration and product handling.

General Manufacturing
Parts, cases, pallets, assembly processes and production-line material flow.
Warehousing & Distribution
Case and tote transport, accumulation, sortation, pallet handling and shipping.
One Integrated Solution Connecting Your Entire Operation
Our material handling experts integrate conveyors with other automated solutions to keep products moving efficiently.


Automated Storage Systems
Connect conveyor systems with automated pallet storage and retrieval systems.

Controls & Software
Controls, programming, and WCS/WES solutions that coordinate equipment and product flow.

Conveyors Designed for Your Products, Process, & Facility
The right conveyor system depends on more than what you’re moving. We engineer systems around how products need to move through your operation today and as your needs change.
✓ Product size, weight & characteristics
✓ Throughput & accumulation requirements
✓ Facility layout & available space
✓ Infeed, discharge & transfer points
✓ Existing equipment & controls
✓ Future growth & expansion
How Conveyors Support Larger Automation Projects
Integrated Material Handling System Streamlines Case Flow for New Beef Plant
Schmeeckle Brothers Construction was selected to build a new 556,000-square-foot beef processing facility for Sustainable Beef in North Platte, Nebraska.
As an industrial contractor specializing in beef processing facilities, Schmeeckle needed a systems partner like RMH Systems that could work within its design-build approach and take responsibility for significant portions of the project.
Challenges
- Coordinating material flow across multiple facility levels
- Moving empty and filled cases efficiently between production areas
- Managing sorting, sealing, merging, and transport to the box cooler
- Integrating equipment from multiple manufacturers into one coordinated system
- Incorporating storage racking into the box cooler design
- Minimizing manual handling and operator interaction between processes
Solutions
RMH worked alongside Schmeeckle to bring multiple technologies together into one coordinated, turnkey material handling and automation system.
The project included:
- Conveyor systems – Custom conveying and case-transfer systems move cases between levels and through multiple stages of the operation.
- Automated case forming – Case-forming equipment is integrated with the conveyor system to automatically supply cases to the production area.
- Sorting & merging – Filled cases return to the upper level for sorting before multiple conveyor lines merge into a single flow.
- Automated case sealing – Case sealing is integrated into the material flow before finished cases continue to the box cooler.
- Warehouse racking – Storage racking supports finished product storage within the facility’s box cooler.
- Controls – Controls and programming coordinate conveyors, case handling equipment, and other automated systems across the operation.
- Truck scales – Truck scales were integrated into the facility to support vehicle weighing.
Results
✓ Automated case flow across multiple facility levels and production areas
✓ Reduced manual handling between process steps
✓ Reduced operator interaction between process steps
✓ Created a coordinated flow from case forming through finished product storage


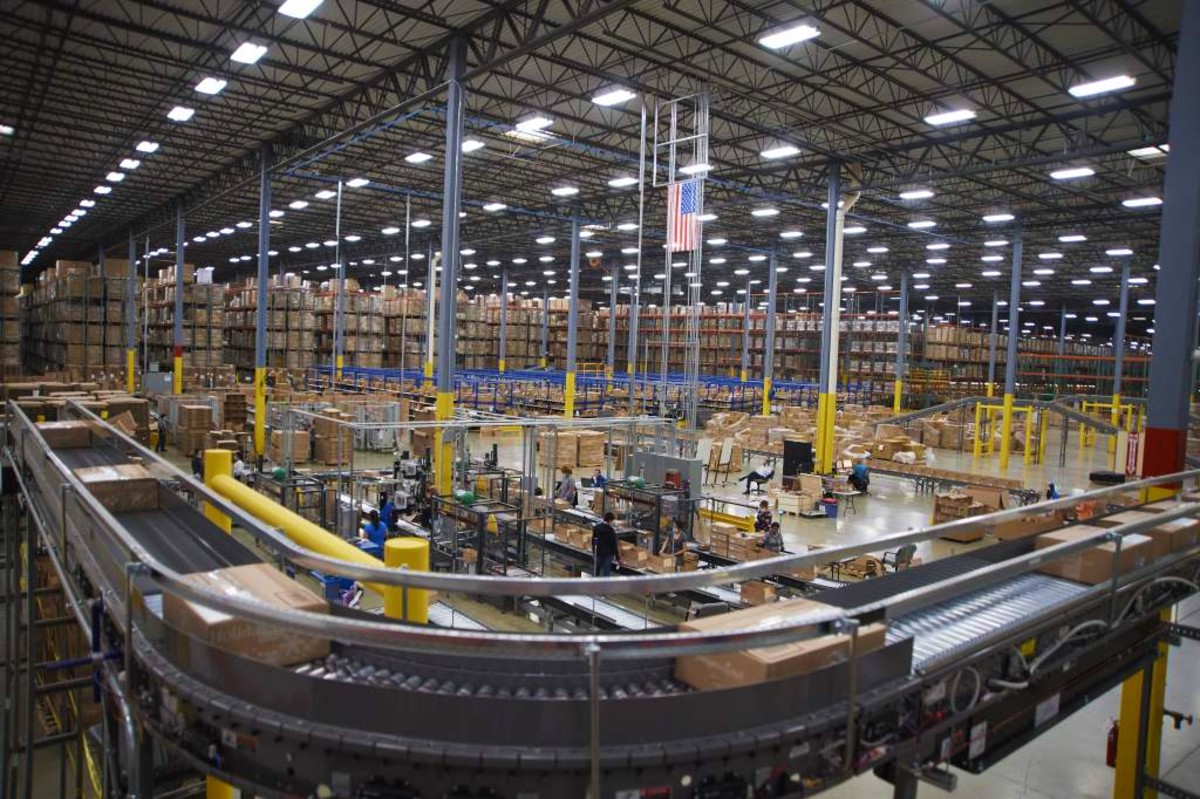
Fulfillment Automation Increases Capacity to Meet Surging Order Demand
During the pandemic, a surge in consumer demand left a major household goods distributor struggling to keep up with orders. The company’s existing fulfillment process couldn’t handle the increased volume, resulting in an order backlog of nearly three months.
The distributor needed to significantly increase fulfillment capacity while creating a more efficient, scalable process for picking, packing, and shipping customer orders.
Challenges
- Nearly three-month order backlog
- Rapid increase in order volume
- Existing fulfillment process unable to keep pace
- Too many manual touches throughout fulfillment
- Need for greater long-term capacity and scalability
Solutions
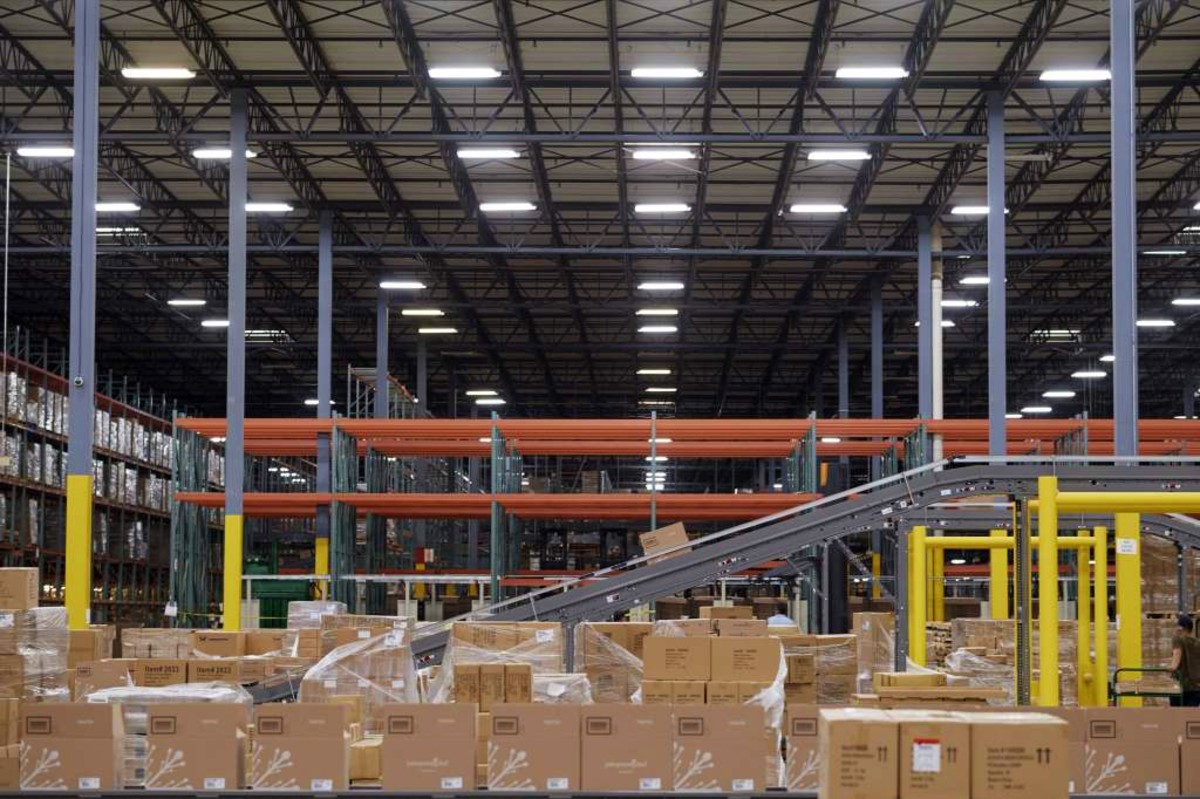
RMH Systems designed and implemented a complete automated order fulfillment system for the company’s 600,000-square-foot distribution facility in the Chicago area.
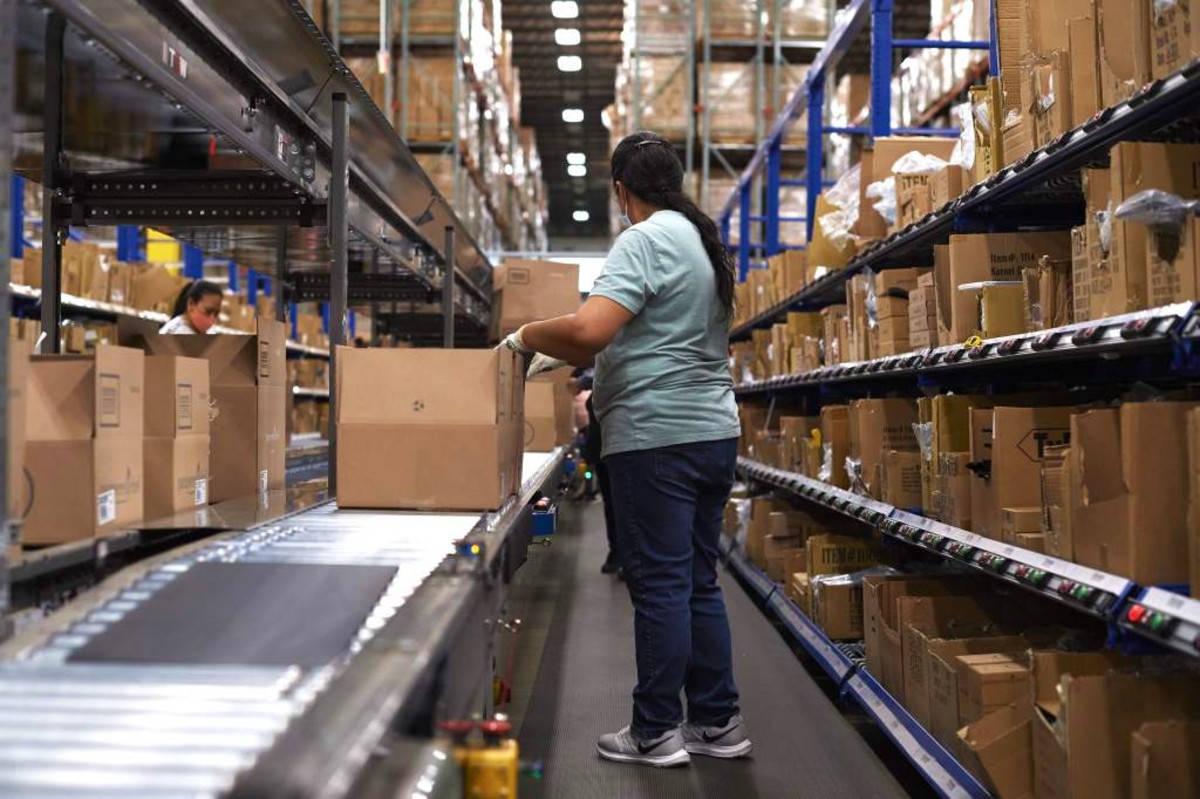
The solution included three carton-flow pick modules and an integrated order-picking system connected to automated packaging and shipping conveyors.
Automation was incorporated throughout the fulfillment process, including:
- Carton erecting
- Pick-to-light technology
- Multi-level conveyors, accumulation, and sortation
- Print-and-apply labeling
- Automatic carton sealing
- Racking, including selective, double-deep, carton flow, and over dock door
By integrating these technologies into one complete system, RMH created a streamlined process that moved orders from picking through packaging and shipping with fewer manual touches.
Results
✓ Increased order fulfillment capacity
✓ Reduced manual handling
✓ Faster movement from picking through shipping production and packaging
✓ More efficient packaging and shipping
✓ Greater ability to handle fluctuations in order volume
✓ Scalable system designed to support future growth
Conveyor Integration Reduces Manual Packing While Reusing Existing Equipment
This customer is a private-label bakery for a major regional grocery store chain. They needed to increase production volume while reducing the manual labor required to pack baked goods into cases.
Challenges
- Increasing production volumes: The bakery needed to support higher production volumes with a process that relied heavily on manual case packing.
- Existing equipment integration: The customer wanted to reuse its existing bulk packer, labeling, case sealing, and palletizing equipment as part of the automated process.
Solutions
RMH designed a conveyor system that integrated with the bakery’s existing packaging equipment, allowing the customer to automate more of the case-packing process while using equipment already in its facility.
Product is conveyed from the flash freezer to an elevated infeed on the customer’s bulk packer, which counts the individual baked goods and drops the appropriate quantity into a case below. A zero-pressure accumulation conveyor automatically indexes cases into position beneath the packer and holds each case in place during filling.
Once a case is filled, the bulk packer signals the conveyor to release it. The case then moves through a case shaker to settle the product before continuing to the customer’s existing labeling, case sealing, and palletizing equipment.
The system also includes a manual packing option that allows product to be diverted to operators if the automated packing process is unavailable, helping the bakery maintain production.
In addition to the conveyor hardware, RMH provided the controls package, which included a control panel, PLC programming, and commissioning to operate the system as one complete solution.
Results
✓ Supports increased production volumes
✓ Reduces repetitive manual case packing
✓ Repurposes employees to higher-value roles
✓ Reuses existing packaging equipment
✓ Maintains flexibility with a manual packing option
Solving Palletless Handling with Custom Conveyor Integration
When growing demand created a need for automated palletizing, this sunflower seed processor faced an unusual challenge: finished loads needed to travel through the system on corrugated slip sheets without pallet support.
Complete Solution Robotics, an RMH System company, partnered with Alba Manufacturing to develop a custom turntable solution that provides smooth transfers, load stability, and reliable handling throughout the system.
See the system in action as it handles palletless loads.

