Top-Running Cranes
Talk with a Crane Expert
Built for Higher Capacities & Longer Spans
Top-running cranes travel on rails mounted above the runway beams. This means they can support higher capacities and longer spans while maximizing available overhead space in your facility.
This configuration provides several advantages for larger lifting applications.

Engineered for Your Lifting Requirements
Top-running cranes are available in single- and double-girder configurations. The right design depends on your load, span, duty cycle, and facility.

Single-Girder Top-Running Cranes
Single-girder cranes use one bridge girder to support the hoist and trolley. They’re an efficient, cost-effective option when the required capacity, span, and duty cycle don’t call for a double-girder system.
Best Fit:
✓ Moderate capacities
✓ Shorter spans
Double-Girder Top-Running Cranes
Double-girder cranes use two bridge girders to support the hoist and trolley. They’re well-suited for applications requiring higher lifting capacities, longer spans, and more demanding duty cycles.
Best Fit:
✓ Higher lifting capacities
✓ Longer spans
✓ Heavy-duty or frequent lifting applications

Lifting Solutions Designed Around Your Facility
A top-running crane has to work with your building as well as your lifting requirements. Our team considers the complete system when designing your crane.

Runway & Structure
Building structure, runway design, and support requirements.

Capacity & Span
Load requirements and the area the crane needs to cover.

Hook Height & Clearance
Available vertical space and required lifting height.

Duty Cycle
How frequently the crane operates and the application demands.

Load Handling
Vacuum lifters, magnets, grabs, or spreader bars, depending on the material being handled.

Controls
Pendant, radio, and other control requirements.
See Our Top-Running Cranes in Action
From overcoming facility constraints to improving how heavy materials are handled, see how RMH has solved real lifting challenges for customers.
20+ Crane Systems Increase Capacity by 50% for Industrial Equipment Manufacturer
Scott Equipment is a family-owned manufacturer of industrial processing equipment serving the animal feed, food, chemical, ethanol, and other industrial markets. When the company expanded its Arlington, Minnesota, facility, it turned to RMH Systems to provide the overhead cranes, hoists, and material handling equipment needed to support the additional production space.
Challenges
Scott Equipment’s Arlington facility expansion required a comprehensive lifting solution that could:
- Support a range of manufacturing processes with different load capacities and lifting requirements.
- Accommodate specialized applications, including explosion-proof equipment for the paint booth.
- Transfer products between facilities with monorail systems connecting the new building, existing building, and wash bay.
- Navigate COVID-era supply chain challenges while keeping a large-scale expansion project moving forward.
Solutions
RMH Systems designed and supplied a complete crane and hoist package for the expanded facility, matching each system to the lifting requirements of its specific application.
The project included:
- 12 top-running single-girder 10-ton cranes, each equipped with two 5-ton Harrington chain hoists
- One 5-ton top-running single-girder R&M crane with a wire rope hoist
- One 10-ton top-running single-girder R&M crane with two 5-ton wire rope hoists
- One 20-ton top-running double-girder crane with two 10-ton wire rope hoists
- Two 10-ton Cable King explosion-proof wire rope monorail hoists with Remtron radio controls for the paint booth
- Two 2-ton Gorbel mast-style jib cranes with Harrington chain hoists
- Two 10-ton monorail systems, each with two 5-ton R&M wire rope hoists, to transfer products between the new building, existing facility, and wash bay
Results
✓ 50% more production capacity
✓ Expanded lifting capabilities to support a wider range of manufacturing requirements
✓ Improved product movement between the new building, existing facility, and wash bay
✓ Specialized lifting capabilities for areas such as the paint booth
How 100+ Custom Crane Systems Support Operations at Leading Steel Distributor
For more than 40 years, McNeilus Steel has partnered with RMH Systems to make heavy steel handling safer and more efficient. Across four facilities in Minnesota, North Dakota, Wisconsin, and Tennessee, RMH has provided more than 100 overhead cranes engineered for applications ranging from tubing and plate to 40-ton steel coils.
Challenges
Handling heavy steel products safely and efficiently requires different solutions depending on the material.
McNeilus needed crane systems that could handle everything from steel coils to tubing and plate while reducing labor-intensive material movement and supporting safer processes for employees.
Solutions
Coil Handling: 40-ton Demag double-girder cranes provide the capacity required to lift and move heavy steel coils.
Tubing Handling: 10-ton Demag double-girder cranes with dual hoists help operators handle and position long steel tubing.
Steel Plate Handling: 20-ton Demag double-girder cranes with dual hoists and magnets allow steel plate to be lifted and transported without relying on more labor-intensive handling methods.
Results
✓ Safer material handling by reducing labor-intensive movement of heavy steel products
✓ More efficient plate handling using magnets to lift and transport steel
✓ Application-specific lifting for coils, tubing, and plate
✓ Scalable crane infrastructure supporting operations across four facilities
✓ 100+ cranes installed over a 40-year partnership
Right-Sized Cranes for Complex Production at Fiberglass Composite Manufacturer
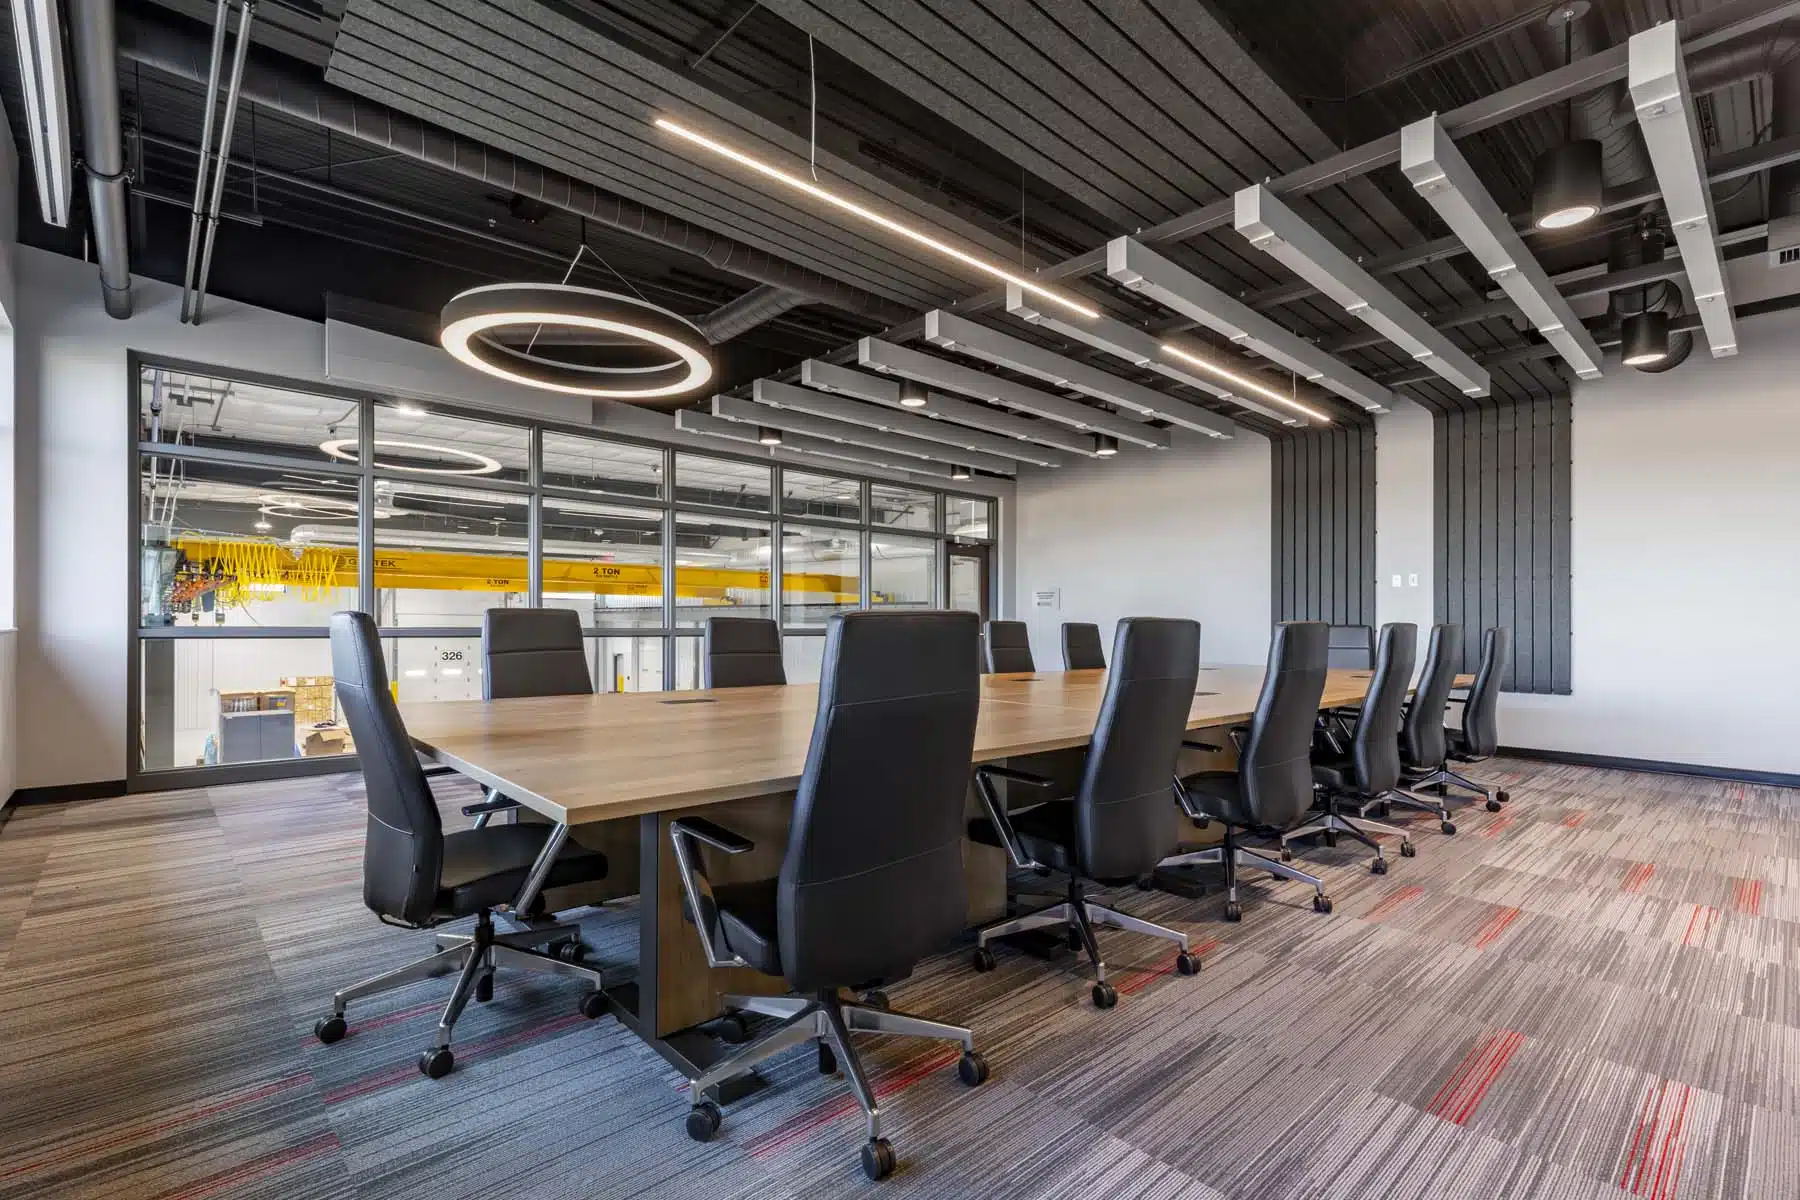
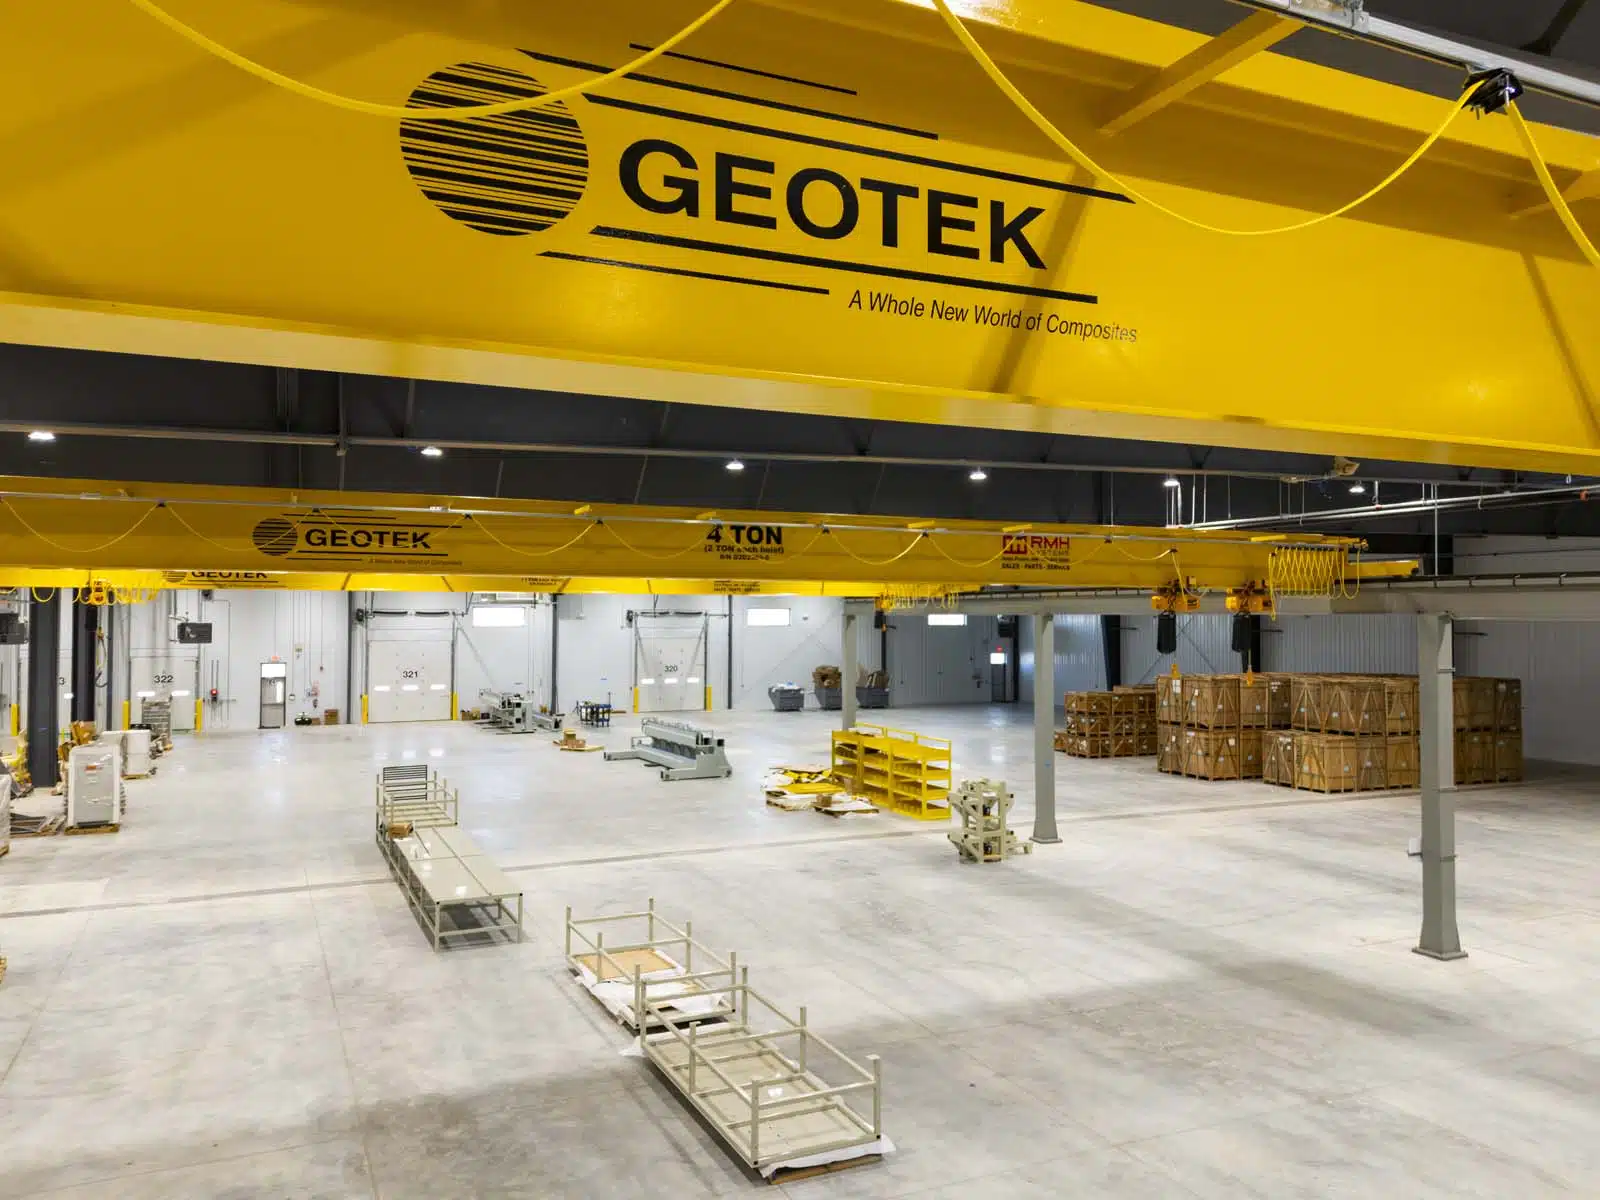
When GEOTEK expanded into fiberglass composite utility pole manufacturing, the company built a new 105,000-square-foot facility in Stewartville, Minnesota. The new operation required overhead cranes that could work within the facility layout while accommodating production equipment, space constraints, and changing lifting requirements.
Project Highlights
✓ Right-sized crane systems with capacities and controls matched to each application
✓ Engineering adjustments to accommodate machine clearances and other facility challenges
✓ Specialized radio controls for precise crane operation
✓ Post-installation tuning to ensure the controls met GEOTEK’s operational needs



One Trusted Partner for Complete Overhead Crane Support
With RMH Systems, you have one team behind your top-running crane from initial design through ongoing support.


